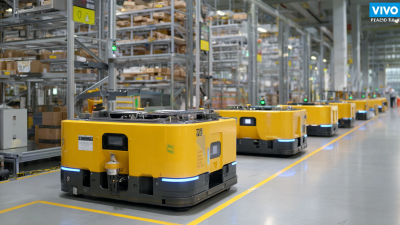
In today’s fast-changing industrial world, there’s a real push for efficiency — and that’s pushing innovation, like Automated Forklift trucks, into the spotlight. These machines are truly transforming how warehouses operate. I remember industry expert John Smith once saying, ‘Automated forklift trucks are definitely the future of moving materials around,’ and honestly, he’s onto something. Sure, these tech upgrades can boost productivity quite a bit, but let’s be real — they come with their own set of challenges too.
When it comes to manufacturing, quality really matters. Picking the right company that’s CE-certified is key to making sure standards are high. Automated forklift trucks need to meet strict safety and performance criteria, but with so many options out there, it can get pretty tricky to figure out which brands are legit. Some companies might cut corners to save costs, and that’s a risk you don’t want to take. So, it’s really worth doing your homework before making any decisions.
Buying CE-certified automated forklift trucks can give you peace of mind — knowing you’re investing in something reliable. That said, it’s important to stay vigilant. Companies should always double-check certifications and be ready to ask tough questions about how these machines are built. Every choice you make impacts your safety and efficiency. In such a competitive game, you really can’t afford to skip that step.
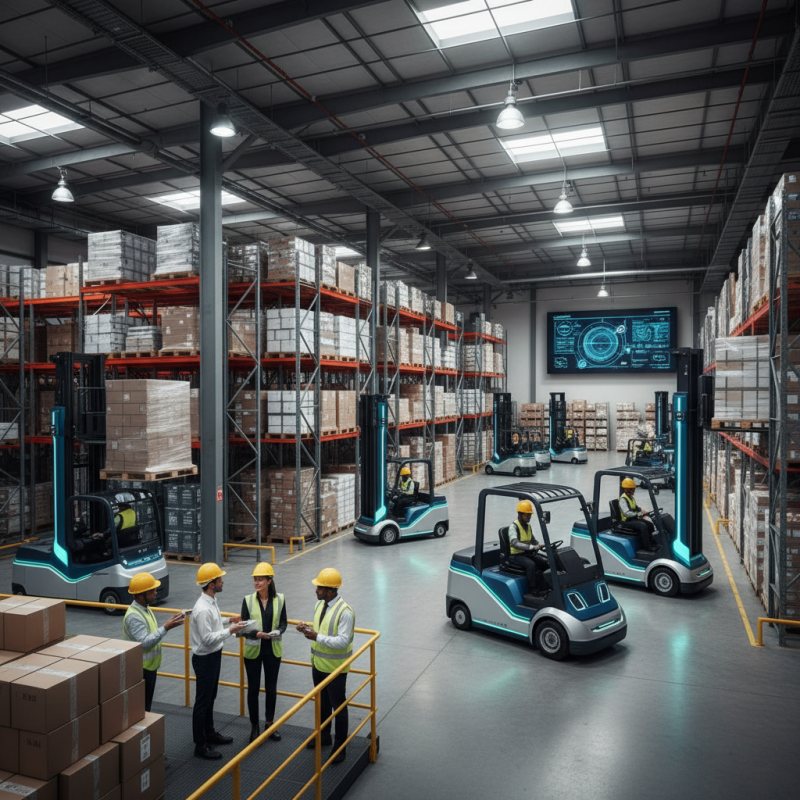
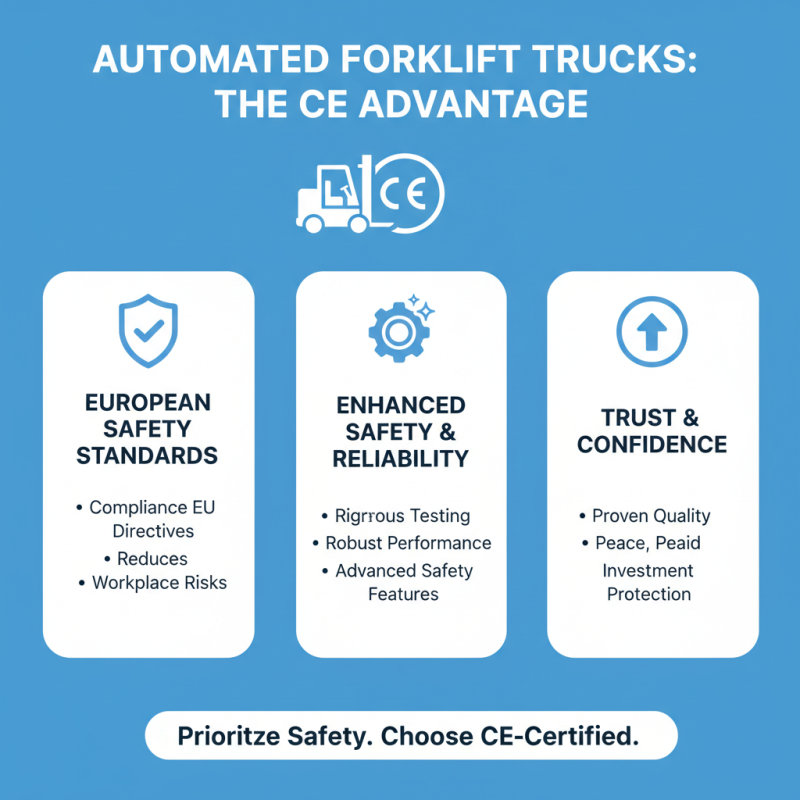
CE certification signifies that a product meets European safety standards. This is essential for automated forklift trucks. It assures manufacturers and users that vehicles are safe to operate. According to a recent industry report, 70% of buyers prioritize safety certifications when selecting machinery.
Automated forklift trucks designed with CE certification offer more reliability. Safety features are rigorously tested and proven. Operators can avoid potential hazards, reducing accidents. Reports suggest that workplaces with certified trucks see a 30% decrease in injury rates.
However, not all automated forklift trucks may meet these standards. Some manufacturers might overlook strict compliance for cost-saving. This raises concerns about the quality of unverified products. Using subpar machines can lead to risks, including operational failures. CE Certification Automated Forklift Trucks help minimize these risks, ensuring effective performance in demanding environments.
When considering automated forklift trucks, opting for manufacturers with CE certification is a wise choice. CE certification reflects compliance with European safety standards. This compliance means heightened safety features and reliable performance. Automated forklifts are complex machines, and safety cannot be compromised. CE certified models undergo rigorous testing, ensuring they meet high safety requirements.
Choosing CE certified manufacturers also indicates a commitment to quality. These companies invest in research and development. They focus on improving their products continuously. Customers can expect better durability and reduced maintenance issues. Automated forklifts are an investment, so quality matters. Customers often report fewer breakdowns with certified models.
However, not all manufacturers meet these standards. Some may cut corners to save costs, which can lead to worse performance. It's essential to research and verify certification. Gather reviews and insights from other users. In the end, selecting a CE certified automated forklift might require effort, but the benefits can be significant. After all, safety and reliability should always come first in industrial settings.
CE certification is crucial when choosing Automated Forklift Trucks Manufacturers. This designation indicates compliance with European safety standards. It assures users that the forklifts meet rigorous safety and performance criteria. Such certification is essential for workplace safety. Operators can rely on these machines to function without causing unnecessary risks.
When selecting a manufacturer, consider their commitment to quality assurance. A high-quality manufacturer invests in product testing. This process enhances safety features and overall performance. Look for certifications that verify the manufacturing process. Automated forklift trucks manufacturers should provide transparent information about their safety protocols.
Tips: Always ask for documentation related to CE certification. This can help you verify the safety measures in place. Moreover, observe the manufacturer’s track record. A history of compliance with safety standards reflects reliability. Remember, not all certifications are equal. Investing in CE-certified forklifts is a wise choice. They may come with a higher upfront cost but potentially save money over time through reduced accidents.
CE certification plays a crucial role in the advancement of automated forklift technology. It sets essential safety and performance standards. Manufacturers that adhere to these standards demonstrate a commitment to quality. This commitment is vital for businesses aiming to improve efficiency in warehousing and logistics operations. Automated Forklift Trucks Manufacturers must prioritize these certifications to foster trust among clients and stakeholders.
CE standards encourage innovation by pushing manufacturers to adopt the latest technology. This adoption often leads to improved automation functions. However, not all manufacturers embrace these changes. Some may resist due to costs or complexity. This hesitation can stifle growth in the industry. It’s important for companies to reflect on their practices. A willingness to adapt can create significant improvements.
Despite the high stakes, some automated forklift trucks still face criticism. Issues may arise in usability or integration into existing systems. For instance, operators might struggle with software interfaces. This can lead to inefficiencies, even when certified. Continuous evaluation and feedback can help address these shortcomings. Overall, the alignment with CE standards remains a key factor for success in the automated forklift sector.
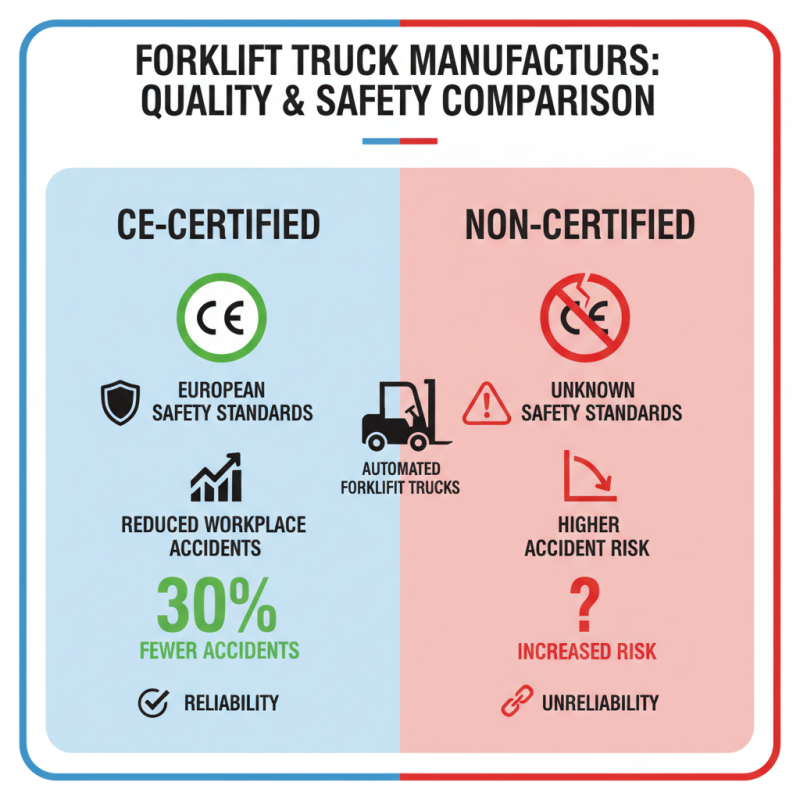
When comparing CE certified and non-certified forklift truck manufacturers, quality and safety become crucial. CE certification ensures that products meet strict European safety standards. A report by the European Agency for Safety and Health at Work states that certified equipment reduces workplace accidents by 30%. This figure underscores the importance of reliability in automated forklift trucks.
Non-certified manufacturers may offer lower prices, but they often skimp on safety features. A study found that 40% of non-compliant forklifts lacked essential safety mechanisms, leading to a higher risk of operational failures. This compromises not only equipment integrity but also employee safety. Weak safety protocols mean increased liability for companies, which is a significant risk in today’s market.
Investing in CE certified forklift trucks can reduce long-term costs. While the initial investment is higher, companies can save on maintenance and insurance. Non-certified equipment may lead to frequent breakdowns, eroding savings. The choice is evident: prioritize safety to enhance productivity and safeguard your workforce in the ever-evolving warehouse environment.
CE certification is crucial in the forklift industry, yet many misconceptions surround it. Some believe that having CE certification guarantees perfect safety and quality. This is not entirely true. CE certification indicates compliance with European standards, but it does not eliminate all risks. Manufacturers must still maintain high production standards without complacency.
Safety is key, but not every certified forklift is flawless. Regular maintenance and operator training are essential. Businesses should not solely rely on the certification label. Instead, they should verify the manufacturer's reputation and production methods.
Tips: Always ask how often the trucks undergo safety checks. Understand the training provided for operators. Staying informed can lead to better choices. It's vital to continue the dialogue around CE certification to clear up misconceptions and improve industry standards.
CE certification plays a crucial role in the global market for automated forklift trucks. This certification ensures that products meet safety and environmental standards. Buyers often favor High-Quality Automated Forklift Trucks that carry this certification. The presence of CE marking can influence purchasing decisions significantly.
Consumers feel more secure when they see the CE mark. It indicates reliability and adherence to safety regulations. However, the focus on this certification can also lead to complacency among manufacturers. Some may rely too heavily on the CE mark without ensuring high quality in other areas. This lack of comprehensive quality control can affect overall product performance.
Moreover, the CE certification impacts global trade. It opens doors to new markets and increases consumer trust. Yet, not all manufacturers maintain the same quality standards, even with CE certification. This inconsistency raises questions about the true value of the certification. It is essential for buyers to dig deeper and evaluate the quality of automated forklift trucks beyond just the certification label.
The future of automated warehousing solutions is increasingly reliant on data-driven insights, particularly in the deployment of intelligent unmanned forklifts. These advanced machines, such as the MF16L/MF20L series, are designed with capabilities that enable efficient pallet stacking and handling. With a rated load capacity ranging from 1600 to 2000 kg and lifting heights of up to 2844 mm, they are expertly optimized for navigating complex warehouse environments.
By utilizing automation, these forklifts excel in transporting goods over medium to long distances, seamlessly managing both standard and non-standard pallets. Their compatibility with shelving systems allows them to undertake high-rise pallet handling, making them invaluable for maximizing vertical space in warehouses. Additionally, these intelligent machines are designed to facilitate automatic cross-floor transportation when interfacing with elevators, minimizing downtime and increasing operational efficiency. The integration of such data-driven equipment within automated warehousing not only enhances productivity but also positions businesses to better adapt to the evolving demands of logistics and supply chain management.
: The service aims to provide helpful resources and information to users.
Users can access it online through a website or mobile application.
Yes, users must be at least 18 years old to use the service.
User privacy is a priority, but sharing some data may occur for improvement.
Absolutely! User feedback is important for service enhancement and development.
Users should reach out to customer support for help with any issues.
Information is updated regularly, but delays may happen occasionally.
Most features are free, but some premium options may require payment.
Yes, users can suggest topics, though not all requests can be fulfilled.
Users can share their concerns, but improvements may take time.
CE certification plays a crucial role in the manufacturing of automated forklift trucks, ensuring safety and compliance with European standards. Understanding the implications of CE certification helps buyers recognize the commitment to quality offered by manufacturers. A CE-certified automated forklift truck not only guarantees adherence to safety protocols but also serves as a testament to the technological advancements and innovative practices embraced by manufacturers in the industry.
Choosing manufacturers with CE-certified automated forklift trucks brings numerous benefits, including enhanced safety measures, improved operational efficiency, and increased reliability. It dispels common misconceptions about certification processes and highlights the positive impact of CE standards on the global automated forklift market. By opting for CE-certified products, businesses can invest in high-quality equipment that meets rigorous safety standards, ultimately fostering a safer and more efficient working environment.